


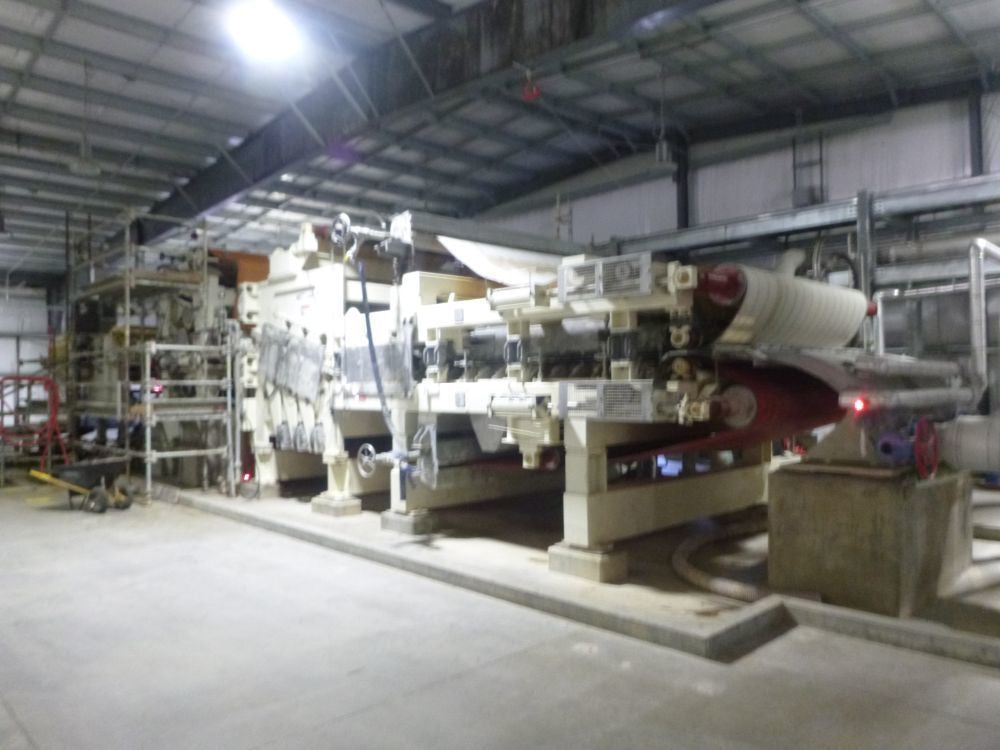


Used 2.5 m Hymac Press Technologies Wetlap Machine, 100 HP-8F, Rebuilt 2018
Used 2.5 m Hymac Press Technologies Wetlap Machine, 100 HP-8F, Rebuilt 2018In stock · 1
- LTL freight quoted by destination
- PO and tax-exempt orders accepted
- 30-day returns
- Same-day processing
- Questions on fit or specs: (612) 449-0646
Specification
as recorded from the nameplate
- Condition
- Used What our grades mean
- Manufacturer
- Hymac (twin wire press and cutter layboy) and Press Technologies (heavy-duty secondary press and 2018 rebuild)
- Line
- 2.5 m (100 in) wetlap line: twin wire press, heavy-duty secondary press, and cutter layboy
- Primary press
- Hymac Model 100 HP-8F twin wire wet-lap press. A short listing also writes this as 100 HP-SF; the builder documents use 100 HP-8F.
- Secondary press
- Press Technologies Model 100 HDP heavy-duty twin wire secondary press. Builder drawings also call this the 100 in HDP.
- Cutter layboy
- Hymac Model 100 CLB (also written 100-CLB) cutter layboy, with knife-entry belt, rotary fly knife, vacuum sheet transfer, scissors-lift stacker, and discharge conveyors
- Width
- 2.5 m (100 in), as used in the builder drawings for this line
- Rebuild
- Line rebuilt by Press Technologies in 2018. The 100 HDP secondary press was supplied new at that time and designed to run with the rebuilt Hymac press and cutter layboy.
- Rated capacity
- 200-400 TPD, as stated on the short listing
- Desired capacity when installed
- 400 ODSTPD (the original Hymac duty, before this rebuild, was listed at 100 ODSTPD on groundwood)
- Specified furnish, 2018
- Non-wood (wheat straw) for the 2018 duty. The original Hymac duty had been groundwood.
- Inlet consistency
- 3.5-4.5% OD (the original Hymac duty was listed at 4-5% OD)
- Discharge consistency
- The short listing states 45+2% OD, which matches the 2018 rebuild target of 45 ± 2% OD for the line. The HDP secondary-press application was written for 49 ± 2% OD. The HDP write-up says the secondary nip commonly raises consistency about 4-6% or more, depending on operating conditions. The original Hymac duty was listed at 47% OD. Confirm the expected discharge for your furnish at inspection.
- Temperature
- ≥ 130 F, as specified for the 2018 duty
- Ph, 2018 duty
- Specified at 11-12 (the original Hymac duty was listed at 6.5-7.5)
- Primary press dewatering
- Wedge (forming) zone with HDPE drainage plates and a YV side-deckle seal, adjustable about 0-5 degrees; S-roll section; then a high-pressure nip section with three pairs of non-driven nip rolls and one pair of nipped drive rolls
- Primary nip load
- Adjustable 0-1,000 PLI, with typical operating pressures listed at 100-900 PLI. The rebuild specification also describes gradually increasing loads through the three nips, likely 200-800 PLI under typical conditions.
- Primary drive
- Single motor with a dual-output gearbox driving the nipped drive rolls, listed as a 125 HP variable-speed AC drive. Confirm the installed motor and nameplate at inspection.
- HDP nip load
- Pneumatic loading with Firestone air bags, performance design pressure up to 1,200 PLI
- HDP drive
- Two 40 HP AC motors, dual drive, on two rubber-coated driven press rolls. Gearboxes, drive shafts, and sole plates were included with the HDP.
- HDP water
- 60 USGPM; 125 PSI recommended, 80 PSI minimum, fresh or filtered water recommended
- HDP air
- 10 CFH average, 200 CFH at inflation; 125 PSI recommended, 80 PSI minimum
- Belts
- Twin wire (upper and lower) on both the primary press and the HDP. Cantilever frames accept endless or seamed belts. Automatic pneumatic tensioning and tracking, with belt-overtrack shutdown, and belt showers on both units.
- Cutter
- Rotary fly knife against a fixed anvil. Knife speed sets sheet length and then follows line speed. High-pressure water split and trim for side trim and a center cut. Vacuum pick-up belt carries cut sheets to the stacker.
- Stacker
- Hydraulic scissors-lift stacking table with optic sensors, pneumatically operated forks, discharge conveyors, and a scale base at the pick-up point. A dedicated hydraulic power unit is shown in the photographs.
- Controls
- New electrical and control system as part of the 2018 rebuild. Photographs show a Hymac stainless control cabinet with pneumatic gauges and an HMI panel tagged HM-501, plus a local pneumatic cabinet.
- Section weights, drawing labels
- From the 2017 foundation drawing: headbox 5,500 lb; table frame 66,000 lb; main press 100,000 lb; 100 in HDP 62,400 lb; cutter roll assembly 26,970 lb; fork assembly 8,750 lb. These are drawing labels, not a weighed as-installed total. Confirm before you plan the lift.
- Overall length
- Shown on the foundation plan and elevation. We can review the drawing with serious inquiries. Confirm overall length, width, and lift plan at inspection.
- Quantity available
- 1
- Listed
Request a quote
Request a quote for this unit
Tell us the quantity and when you need it. You get a written quote with price, availability and freight to your dock, ready for your PO, within 24–48 hours.
Prefer to talk? Call (612) 449-0646
Details
Product Description
Product Description
Used 2.5 m (100 in) Hymac and Press Technologies wetlap line, completely rebuilt in 2018, with a new electrical and control system. The line is a Hymac Model 100 HP-8F twin wire press, a Press Technologies Model 100 HDP heavy-duty secondary press, and a Hymac Model 100 cutter layboy. A short listing also writes the Hymac model as 100 HP-SF; the builder documents use 100 HP-8F. The short listing rates the machine at 200-400 TPD, with a desired capacity when installed of 400 ODSTPD. Inlet consistency is 3.5-4.5% OD. Discharge is listed at 45 ± 2% OD, and the HDP application was written for 49 ± 2% OD.
Key Specifications
| Specification | Detail |
|---|---|
| Manufacturer | Hymac (twin wire press and cutter layboy) and Press Technologies (heavy-duty secondary press and 2018 rebuild) |
| Line | 2.5 m (100 in) wetlap line: twin wire press, heavy-duty secondary press, and cutter layboy |
| Primary Press | Hymac Model 100 HP-8F twin wire wet-lap press. A short listing also writes this as 100 HP-SF; the builder documents use 100 HP-8F. |
| Secondary Press | Press Technologies Model 100 HDP heavy-duty twin wire secondary press. Builder drawings also call this the 100 in HDP. |
| Cutter Layboy | Hymac Model 100 CLB (also written 100-CLB) cutter layboy, with knife-entry belt, rotary fly knife, vacuum sheet transfer, scissors-lift stacker, and discharge conveyors |
| Width | 2.5 m (100 in), as used in the builder drawings for this line |
| Condition | Used, completely rebuilt in 2018, with a new electrical and control system |
| Rebuild | Line rebuilt by Press Technologies in 2018. The 100 HDP secondary press was supplied new at that time and designed to run with the rebuilt Hymac press and cutter layboy. |
| Rated Capacity | 200-400 TPD, as stated on the short listing |
| Desired Capacity When Installed | 400 ODSTPD (the original Hymac duty, before this rebuild, was listed at 100 ODSTPD on groundwood) |
| Specified Furnish, 2018 | Non-wood (wheat straw) for the 2018 duty. The original Hymac duty had been groundwood. |
| Inlet Consistency | 3.5-4.5% OD (the original Hymac duty was listed at 4-5% OD) |
| Discharge Consistency | The short listing states 45+2% OD, which matches the 2018 rebuild target of 45 ± 2% OD for the line. The HDP secondary-press application was written for 49 ± 2% OD. The HDP write-up says the secondary nip commonly raises consistency about 4-6% or more, depending on operating conditions. The original Hymac duty was listed at 47% OD. Confirm the expected discharge for your furnish at inspection. |
| Temperature | ≥ 130 F, as specified for the 2018 duty |
| pH, 2018 Duty | Specified at 11-12 (the original Hymac duty was listed at 6.5-7.5) |
| Primary Press Dewatering | Wedge (forming) zone with HDPE drainage plates and a YV side-deckle seal, adjustable about 0-5 degrees; S-roll section; then a high-pressure nip section with three pairs of non-driven nip rolls and one pair of nipped drive rolls |
| Primary Nip Load | Adjustable 0-1,000 PLI, with typical operating pressures listed at 100-900 PLI. The rebuild specification also describes gradually increasing loads through the three nips, likely 200-800 PLI under typical conditions. |
| Primary Drive | Single motor with a dual-output gearbox driving the nipped drive rolls, listed as a 125 HP variable-speed AC drive. Confirm the installed motor and nameplate at inspection. |
| HDP Nip Load | Pneumatic loading with Firestone air bags, performance design pressure up to 1,200 PLI |
| HDP Drive | Two 40 HP AC motors, dual drive, on two rubber-coated driven press rolls. Gearboxes, drive shafts, and sole plates were included with the HDP. |
| HDP Water | 60 USGPM; 125 PSI recommended, 80 PSI minimum, fresh or filtered water recommended |
| HDP Air | 10 CFH average, 200 CFH at inflation; 125 PSI recommended, 80 PSI minimum |
| Belts | Twin wire (upper and lower) on both the primary press and the HDP. Cantilever frames accept endless or seamed belts. Automatic pneumatic tensioning and tracking, with belt-overtrack shutdown, and belt showers on both units. |
| Cutter | Rotary fly knife against a fixed anvil. Knife speed sets sheet length and then follows line speed. High-pressure water split and trim for side trim and a center cut. Vacuum pick-up belt carries cut sheets to the stacker. |
| Stacker | Hydraulic scissors-lift stacking table with optic sensors, pneumatically operated forks, discharge conveyors, and a scale base at the pick-up point. A dedicated hydraulic power unit is shown in the photographs. |
| Controls | New electrical and control system as part of the 2018 rebuild. Photographs show a Hymac stainless control cabinet with pneumatic gauges and an HMI panel tagged HM-501, plus a local pneumatic cabinet. |
| Section Weights, Drawing Labels | From the 2017 foundation drawing: headbox 5,500 lb; table frame 66,000 lb; main press 100,000 lb; 100 in HDP 62,400 lb; cutter roll assembly 26,970 lb; fork assembly 8,750 lb. These are drawing labels, not a weighed as-installed total. Confirm before you plan the lift. |
| Overall Length | Shown on the foundation plan and elevation. We can review the drawing with serious inquiries. Confirm overall length, width, and lift plan at inspection. |
| Quantity Available | 1 |
Specifications are taken from nameplates, builder sheets, and available records for this machine. Where a record conflicts with a short listing summary, the source sheet is used and the difference is noted below. Contact us to confirm fitment for your grades and mill before you commit.
What This Machine Is
This is a used 2.5 m (100 in) wetlap line: a Hymac Model 100 HP-8F twin wire press, a Press Technologies Model 100 HDP heavy-duty secondary press, and a Hymac Model 100 cutter layboy. The short listing also writes the Hymac model as 100 HP-SF. The purchase documents and rebuild specification use 100 HP-8F, and that is the designation used here.
The line was completely rebuilt by Press Technologies in 2018, with a new electrical and control system. The 100 HDP secondary press was supplied new at that time, to run with the rebuilt Hymac press and cutter layboy. After the primary twin wire press, the thickened sheet transfers onto the bottom wire of the HDP, is carried into the large press nips, and can then go to the cutter layboy, to a drying line, or to another discharge arrangement.
The short listing rates the machine at 200-400 TPD, with a desired capacity when installed of 400 ODSTPD. That 400 ODSTPD figure is the 2018 rebuild target. The original Hymac duty, before this rebuild, was listed at 100 ODSTPD on groundwood. The 2018 process conditions were written for a wheat-straw furnish at 3.5-4.5% OD inlet consistency, a discharge target of 45 ± 2% OD, temperature of 130 F or higher, and pH of 11-12. Confirm furnish, rate, and expected dryness at inspection.
Hymac Model 100 HP-8F Twin Wire Press
The Hymac Model 100 is a cantilever twin wire press that dewaters pulp between two endless, porous synthetic belts. The belts are supported by dewatering plates and free-turning rollers. Dewatering is arranged in three continuous zones.
In the wedge, or forming, zone, the sheet is formed as the upper and lower belts converge. Both belts are supported by HDPE drainage plates. The upper plates can be adjusted, and the wedge is described as adjustable from 0-5 degrees, to be set in the field. Side sealing is by a YV urethane deckle seal. The operating manual says the upper and lower plate systems should not come closer than 0.75 in (18 mm) at the end of the wedge unless directed by the builder. This machine also has a floating-wedge modification: the discharge end of the forming section can be pneumatically loaded with air bags, pivoting from the inlet end, with adjustment bolts if that movement is to be limited or taken out.
The S-section then applies higher pressure as the belts pass through a series of S-rolls. The high-pressure zone uses two opposing rolls in a nip. On the Model 100 this is three pairs of non-driven nip rolls and one pair of nipped drive rolls. Nip pressure is adjustable from 0 to 1,000 PLI, with typical operating pressures listed at 100-900 PLI. The rebuild specification describes gradually increasing loads through the three nips, likely 200-800 PLI under typical conditions. Loading is pneumatic, with Firestone air bags and lever arms. Nip pairs are arranged on an upward slope to help shed water from the top belt. Pressate is taken away with fixed doctors and collection pans.
The drive rolls are both driven through a single variable-speed AC drive and a dual-output gearbox, so the upper and lower rolls stay speed-matched. That drive is listed as 125 HP. The headbox is stainless, dual-inlet, and pressurized, with water addition points and deckle attachments. Wetted parts such as the headbox, drain pans, tensioning thrust shafts, shower bars, and enclosures are described as stainless (grade not stated, probably 304 or 316). The frame is painted carbon steel, tubular and heavy plate, cantilevered for endless or seamed belts. Automatic pneumatic tensioning and tracking are fitted on both belts, with a belt-overtrack detector for shutdown, and oscillating AES showers with stainless enclosures.
Press Technologies Model 100 HDP Heavy Duty Secondary Press
The thickened sheet from the primary twin wire press transfers onto the bottom wire of the Press Technologies Model 100 HDP and is carried up into the large press nips. Pressure is applied pneumatically with Firestone air bags, with a performance design pressure up to 1,200 PLI. High-performance roll covers are generally used at these pressures. The moisture removed in the nip will commonly raise consistency about 4-6% or more, depending on operating conditions. Pressate is doctored away into drain pans. After pressing, the sheet travels down to a discharge roll, where it can be transferred to the cutter layboy, sent to a drying line, or handled in some other way.
The HDP is a cantilever twin wire unit for endless or seamed belts. It was specified with two rubber-coated driven press rolls and a dual drive; automatic pneumatic tensioning and tracking on both belts, with a belt-overtrack shutdown; belt showers with stainless enclosures; four rubber-covered deflection rolls; a stainless pressate tray; and a water doctor at the nip. Bearings are spherical roller type, specified with a B-10 life in excess of 100,000 hours (SKF or equal), and a multiple non-contact sealing system. The frame is tubular carbon steel, epoxy coated. The supply included one set of upper and lower belts, two gearboxes, drive shafts, sole plates, and a pneumatic control panel.
The HDP application was written for 400 ODSTPD, 3.5-4.5% OD inlet consistency, and 49 ± 2% OD discharge, at 130 F or higher. Service requirements listed for the HDP are 60 USGPM of water (125 PSI recommended, 80 PSI minimum) and air at 10 CFH average, 200 CFH at inflation (125 PSI recommended, 80 PSI minimum). The motor list is two 40 HP AC motors.
Hymac Model 100 Cutter Layboy
The Model 100 CLB cutter layboy takes the sheet from the HDP, cuts it to length, and stacks it into bales. It has four main sections: the low-speed transfer or knife-entry belt, the cutter knife, the vacuum sheet-transfer system, and the scissors-lift stacking and conveying section.
The knife-entry belt is independently driven and speed-matched to the press. The cutter is a rotary fly knife against a fixed, adjustable anvil. Knife speed is set for the desired sheet length and then tied to press speed so cut length holds as line speed changes. A high-pressure water system provides side trim and a center cut. After the cut, a vacuum pick-up belt carries the sheet over the stacker and drops it onto the stacking table or onto the forks when a bale is being discharged.
The stacking table is a belt conveyor on a hydraulic scissors lift, discharging bales in the machine direction. Optic sensors lower the table as the stack builds. At a set height, pneumatic forks extend to catch incoming sheets while the table lowers and transfers the bale onto a discharge conveyor. That conveyor includes a scale base at the pick-up point. A dedicated hydraulic power unit for the scissors lift is shown in the photographs, along with the discharge conveyors.
Drives, Utilities, and Controls
The primary press drive is listed as a 125 HP variable-speed AC motor with a dual-output gearbox on the nipped drive rolls. The HDP has two 40 HP AC motors. The cutter knife, knife-entry belt, vacuum belt, and discharge conveyors have their own drives, matched to line speed as described above. Confirm nameplates, gearbox ratios, and the electrical supply at inspection.
The short listing states that the line has a new electrical and control system from the 2018 rebuild. Photographs show a Hymac stainless cabinet with a row of pneumatic gauges, an HMI cabinet tagged HM-501, and a smaller pneumatic cabinet beside the cutter. HDP controls were specified to coordinate with the main press and cutter-layboy controls. Utility needs for the HDP are listed above. Confirm air, water, and power at inspection.
Photographs and Documentation
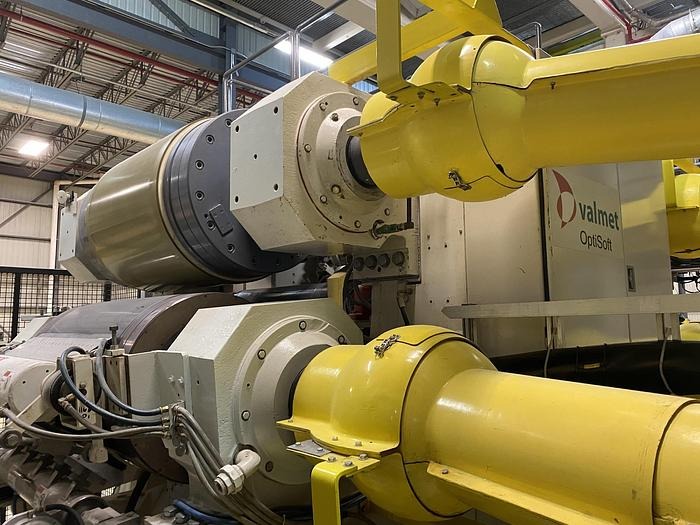
The photographs show the 2.5 m line as it stands: the Hymac twin wire press and Press Technologies HDP, the wet-lap frame and nip guards, roll ends and belt runs, the Hymac control cabinet and HMI, the cutter and knife-entry belt, the discharge conveyors, and the scissors-lift hydraulic unit. One source photograph of a printed layout was left out because it named a prior mill. Confirm what is still mounted with the line, including belts, rolls, the vacuum pick-up, conveyors, the hydraulic unit, and controls, during inspection.
Engineering drawings and rebuild records are available for this line, including a foundation plan and elevation, an HDP general arrangement, and a P&ID and flow schematic. We do not post the raw files with the listing. We can arrange a review for serious inquiries.
What’s Included
This is offered as a used 2.5 m Hymac and Press Technologies wetlap line, completely rebuilt in 2018, as shown in the photographs and described above: the Hymac Model 100 HP-8F twin wire press, the Press Technologies Model 100 HDP secondary press, the Hymac Model 100 cutter layboy with stacking and discharge conveyors, the hydraulic power unit shown, and the electrical and control equipment as installed. Sold as-is. Confirm the exact bill of included equipment, including belts, spare rolls or fabrics, the vacuum pick-up, conveyors, pumps, and controls, during inspection.
Buying Notes
Sold as-is. Inspection by arrangement. Rigging, dismantling, and freight are quoted by item and destination. Used pricing is typically well below new, with a shorter path than buying a new wetlap line of this width. Furnish, expected rate and dryness, belt and roll-cover condition, drives, controls, and what is still with the line should be confirmed on site before you commit.
Frequently Asked Questions
What does 2.5 m refer to, and what is the model number?
2.5 m (100 in) is the line width used in the builder drawings. The Hymac twin wire press is Model 100 HP-8F. A short listing also writes this as 100 HP-SF; the rebuild and purchase documents use 100 HP-8F. The secondary press is a Press Technologies Model 100 HDP, and the cutter layboy is a Hymac Model 100 CLB.
What capacity and dryness can it run?
The short listing rates the line at 200-400 TPD, with a desired capacity when installed of 400 ODSTPD. That 400 ODSTPD figure is the 2018 rebuild target; the original Hymac duty was listed at 100 ODSTPD on groundwood. Inlet consistency is 3.5-4.5% OD. The short listing states a discharge of 45 ± 2% OD, which matches the 2018 rebuild target. The HDP application was written for 49 ± 2% OD. Confirm rate and dryness for your furnish at inspection.
What was included in the 2018 rebuild?
Press Technologies completely rebuilt the line in 2018 and supplied a new 100 HDP secondary press to run with the rebuilt Hymac press and cutter layboy. The short listing also states that the electrical and control system is new. The 2018 process conditions were written for a wheat-straw furnish at 400 ODSTPD. Confirm the present condition of rolls, belts, drives, and controls at inspection.
How is the sheet cut and stacked?
The Hymac Model 100 cutter layboy uses a rotary fly knife against a fixed anvil, with a knife-entry belt, vacuum sheet transfer, and a hydraulic scissors-lift stacker with pneumatic forks and discharge conveyors. A scale base is described at the pick-up point. A hydraulic power unit for the lift is shown in the photographs.
Can the machine be inspected, and how is it sold?
Yes. Inspection is by arrangement. It is sold as-is. Rigging, dismantling, and freight are quoted. We are not an authorized distributor, so the original manufacturer's warranty does not apply.
We are not an authorized distributor, so the manufacturer's warranty does not apply to this unit.
Freight quoted by item & destination.
sales@dwpindustrial.io • (612) 449-0646
Shipping & Handling
Shipping & Handling
$250 flat-rate LTL freight on qualifying orders in the continental US, with overnight, two-day, ground and expedited options available. Hotshot delivery and customer pickup can be arranged.
Orders get same-day processing, Monday–Friday. Transit depends on the carrier and lane.
For international orders or custom shipping needs, please contact us for a quote.
Return Information
Return Information
Return any item within 30 days of delivery.
If the unit is defective or does not match the listing, we pay the return freight and refund or replace it in full. Otherwise the item must be unused and in its original packaging, and you cover the return shipping.
Contact
Contact
Questions on fit, specs, freight or availability? Email sales@dwpindustrial.io or call (612) 449-0646. A person who knows the equipment answers.
Need a different size, voltage or configuration? We source hard-to-find and obsolete equipment through a dealer, factory and surplus network. How sourcing works
Condition and guarantee
We are not an authorized distributor, so the manufacturer's warranty does not apply to this unit. We inspect it, check the nameplate against the listing and photograph the actual unit. If it does not match the description, send it back within 30 days for a full refund. Not sure it fits? Ask us and we will confirm before you order.
More like this in stock


Choose your option


Choose your option

Choose your option


